
Updated: 2026 Engineering Standard · By Sailwin Technical Team
How 100-Point Parison Control Ensures Uniform Wall Thickness in Jerrycans and Detergent Bottles
In modern high-capacity container manufacturing, raw polymer resin accounts for over 60% of total product cost. On older extrusion blow molding machines with static die gaps, operators are forced to increase container weight overall simply to satisfy minimum wall thickness in the thinnest corner or handle section—needlessly wasting hundreds of thousands of dollars in excess plastic.
Overcoming this bottleneck requires dynamic wall thickness regulation throughout the hanging parison. On modern Sailwin extrusion blow molding machines, advanced 100-point servo parison programming (such as MOOG or Rexroth systems) dynamically shifts the die gap in sub-millimeter increments as the tube extrudes.
This engineering guide details the electro-hydraulic mechanics of multi-point parison programming, container geometry thickness profiling, and quantified resin weight savings across commercial container production.
Key Engineering Takeaways
- Dynamic Die Gap Regulation: A high-speed servo hydraulic valve moves the core mandrel up and down across 100 programmable positions along the parison length, allocating thicker plastic to corners and thinner plastic to flat sidewalls.
- Resin Savings of 10% to 18%: By eliminating excess overweight plastic in non-structural container zones, commercial bottlers reduce container gram weight while maintaining top-load stacking strength.
- Drop-Test Survivability: Directing heavier wall thickness into the container pinch-off tail, handle hollows, and bottom corners ensures 100% compliance with UN hazardous transport standards.
Want to Reduce Container Gram Weight Without Losing Strength?
Submit your container drawing (jerrycan, bottle, or drum) for customized 100-point parison profile simulation and resin savings calculations.
1. How 100-Point Parison Control Regulates Container Cross-Sections
Thickness Distribution Rule: A container inflates like a balloon: areas with large expansion ratios become thin; areas with small expansion ratios stay thick. Parison programming pre-compensates for inflation geometry.
Review the parison thickness distribution zones across a standard 5L detergent container:
| Container Section | Expansion Ratio | Parison Point Range | Target Die Gap Position | Structural Function |
|---|---|---|---|---|
| Container Neck & Threads | Low (1.2 : 1) | Points 1 – 15 | Calibrated Medium Gap | Forms rigid neck finish for leak-proof cap sealing. |
| Shoulder & Top Handle | Extreme (3.5 : 1) | Points 16 – 35 | Maximum Open Die Gap | Reinforces hollow handle to prevent rupture when picked up. |
| Main Body Sidewalls | Moderate (2.0 : 1) | Points 36 – 75 | Thinner Tapered Gap | Eliminates overweight plastic on flat labeling panels. |
| Bottom Corners & Pinch | High (3.0 : 1) | Points 76 – 95 | Heavy Enriched Gap | Provides impact resistance during warehouse pallet stacking. |
| Tail Pinch Slug | None (Pinch Waste) | Points 96 – 100 | Reduced Pinch Gap | Minimizes regrind scrap while preserving weld seam strength. |
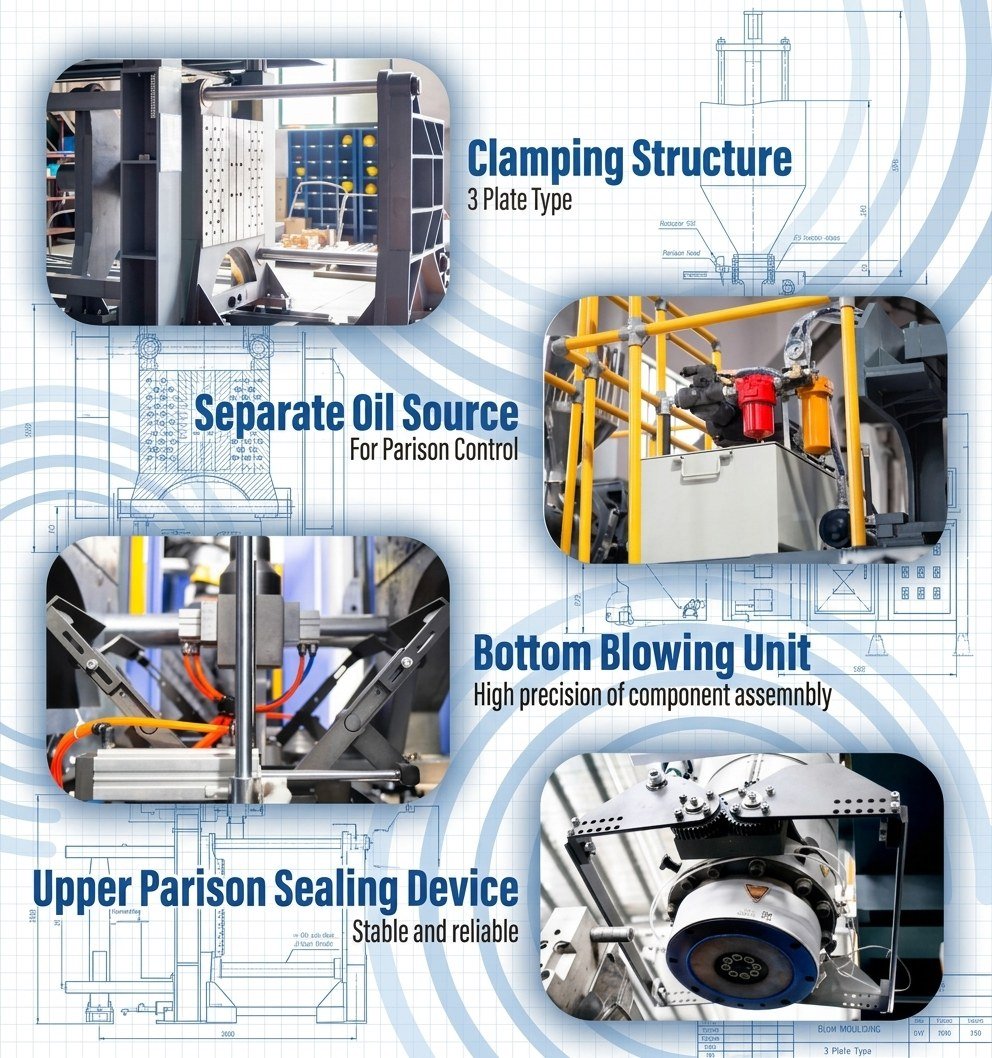
Sailwin Customer Case Study: Jerrycan Manufacturer Cuts Container Weight by 16% While Improving Drop Strength
How a commercial chemical drum molder modernized from fixed-gap die tooling to Sailwin MOOG 100-point parison technology.
- 20L stackable jerrycans required 1,150g weight on older machine to prevent corner cracking.
- High resin consumption cost over $450,000 USD annually on polymer pellets.
- Containers suffered from uneven cooling warpage across asymmetrical handle faces.
- Supplied Sailwin SC-2S25L continuous extrusion blow molding machine equipped with MOOG 100-point parison controller.
- Trained operators to profile parison thickness curves based on 3D container expansion ratios.
- Reinforced bottom corners while shaving wall thickness on flat labeling panels.
- Container net weight safely reduced from 1,150g to 965g (16.1% material reduction).
- Containers successfully passed UN Level I drop tests from 1.9 meters.
- Annual raw material cost savings exceeded $72,500 USD.
Data source: Sailwin Client Quality Audit & Production Log File #SW-EBM-2026, 2026.
Frequently Asked Questions
SAILWIN MACHINERY · FACTORY-DIRECT PACKAGING SYSTEMS
Optimize Container Wall Thickness with Sailwin Engineering
Sailwin integrates world-class MOOG 100-point parison programming on all SC series extrusion blow molding machines. Request factory quote today.
Explore Integrated Packaging Machinery on Sailwin:
• PET Preform Injection Molding Machine – High-speed 140T to 550T systems for multi-cavity bottle preform lines.
• PET Water Bottle Blowing Machine – Linear automatic servo stretch blow molding equipment.
• Liquid Filling Machine & Bottling Line – 3-in-1 rotary monoblocs for drinking water and beverage factories.
• HDPE Extrusion Blow Molding Machine – Industrial continuous blow molding systems for jerrycans and drums.
• Need technical plant advice? Contact our engineering team for free turnkey consultation.



