
Updated: 2026 Engineering Standard · By Sailwin Technical Team
Continuous vs. Accumulator Head Blow Molding: Which Machine for 20L–200L Drums?
When purchasing extrusion blow molding machinery for industrial chemical containers, lubricant barrels, or agricultural tanks, plant managers face a defining architectural choice: should your facility install continuous extrusion blow molding machinery or an accumulator head shot system?
While continuous extrusion excels at high-speed multi-cavity small container production (0.5L to 10L), attempting to continuously extrude heavy 25kg parisons for 200L L-ring drums leads to disastrous parison sagging, neck thinning, and thermal degradation.
This engineering guide analyzes container capacity limits, parison drawdown mechanics, hydraulic clamp tonnages, and capital payback periods across Sailwin heavy-duty EBM production lines.
Key Engineering Takeaways
- Volume Boundary: Continuous extrusion is optimal for containers up to 10L–25L; Accumulator heads are mandatory for heavy containers from 30L to 1,000L IBC intermediate bulk containers.
- Parison Shoot Speed: Accumulator heads store molten plastic in a dedicated internal cylinder, discharging heavy parisons (up to 35kg) in under 2.5 to 4.0 seconds to eliminate gravity draw and sagging.
- First-In First-Out (FIFO): Modern Sailwin accumulator die heads utilize spiral or overlapping FIFO flow channels, preventing polymer stagnation, color change delays, and resin burning.
Need Machine Sizing for Chemical Drums or Tanks?
Submit your container drawing and target resin grade for customized clamping force calculations and accumulator capacity sizing.
1. Direct Engineering Comparison: Continuous Extrusion vs. Accumulator Head
Extrusion Architecture Law: If parison weight exceeds 1.5kg, continuous extrusion cannot overcome gravity sag. Accumulator hydraulic shot cylinders are required to freeze wall thickness integrity.
Review the comprehensive comparison matrix below:
| Technical Dimension | Continuous Extrusion EBM | Accumulator Head EBM | Manufacturing Application |
|---|---|---|---|
| Container Volume Range | 0.1 Liter to 25 Liters | 20 Liters to 1,000+ Liters (IBC tanks) | Accumulator is mandatory for heavy industrial drums. |
| Parison Discharge Method | Continuous steady flow from extruder screw | Intermittent hydraulic ram injection from storage reservoir | Accumulator shoots a 15kg parison in 3 seconds. |
| Parison Sagging Tendency | High on heavy parisons (gravity stretching) | Negligible (parison extruded so fast gravity has no time to act) | Accumulator preserves precise wall thickness. |
| Mold Clamping Movement | Shuttle carriage moves mold under stationary die | Mold remains stationary under descending parison | Stationary molds handle heavy multi-ton drum tooling. |
| Optimal Resins | HDPE, PP, PVC, LDPE (MFI 0.2 – 2.0) | High-Molecular-Weight HDPE (HMW-HDPE MFI < 0.05) | HMW-HDPE delivers superior environmental stress crack resistance. |
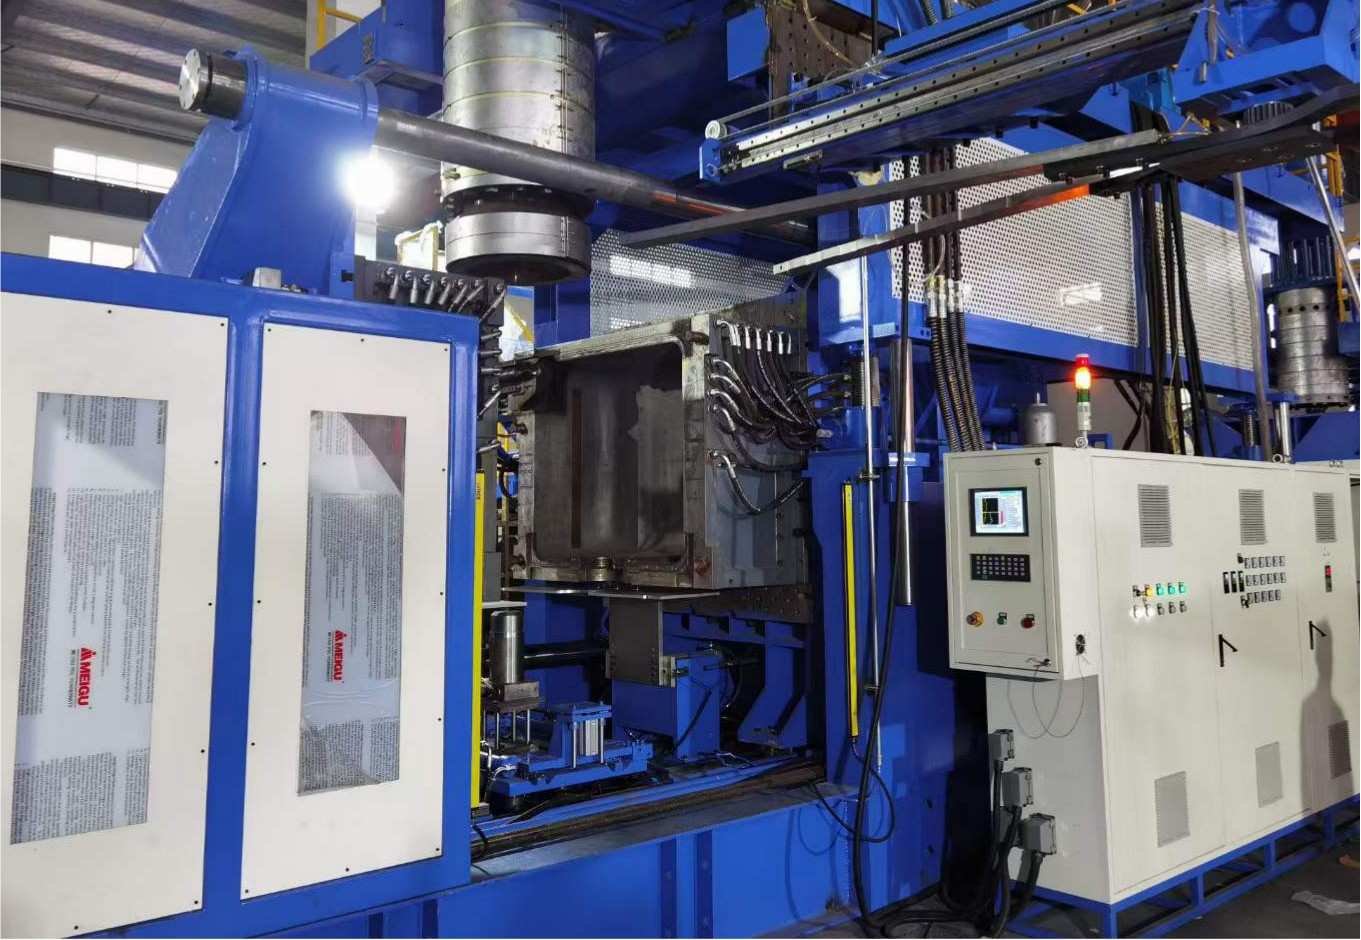
Sailwin Customer Case Study: Industrial Drum Molder Boosts 200L L-Ring Output by 35% with Sailwin Accumulator System
How a commercial chemical barrel manufacturer in the Middle East modernized their 200L packaging line with Sailwin SC-120B accumulator machinery.
- Older machine suffered from weld line delamination during drop tests.
- Slow parison extrusion caused severe top wall thinning and 28% rejection rates.
- Color changeovers between blue and black drums required 6 hours of resin purging.
- Supplied Sailwin SC-120B accumulator blow molding machine featuring a 35L FIFO spiral die head.
- Configured 100-point MOOG parison programming to reinforce chimes and bottom drop rings.
- Integrated dual-circuit high-pressure mold clamping with proportional hydraulic control.
- Drum drop tests passed UN Class 1 hazardous chemical certification from 2.2 meters.
- Total cycle time slashed from 115 seconds to 78 seconds (32.1% output increase).
- Color purge times reduced from 6 hours to 45 minutes with FIFO flow design.
Data source: Sailwin Factory FAT Report & UN Packaging Compliance Audit #SW-200L-2026, 2026.
Frequently Asked Questions
SAILWIN MACHINERY · FACTORY-DIRECT PACKAGING SYSTEMS
Configure Your Heavy-Duty Blow Molding Line with Sailwin
Sailwin manufactures large-scale accumulator head blow molding systems up to 1,000L IBC capacity. Request turnkey consultation today.
Explore Integrated Packaging Machinery on Sailwin:
• PET Preform Injection Molding Machine – High-speed 140T to 550T systems for multi-cavity bottle preform lines.
• PET Water Bottle Blowing Machine – Linear automatic servo stretch blow molding equipment.
• Liquid Filling Machine & Bottling Line – 3-in-1 rotary monoblocs for drinking water and beverage factories.
• HDPE Extrusion Blow Molding Machine – Industrial continuous blow molding systems for jerrycans and drums.
• Need technical plant advice? Contact our engineering team for free turnkey consultation.



