
Updated: 2026 Engineering Standard · By Sailwin Technical Team
Why Do PET Bottles Have Pearlescence and Hazing? Preform Heating & Stretch Rod Troubleshooting
In commercial PET stretch blow molding, container optical clarity is the hallmark of brand quality. When finished water or beverage bottles emerge from the blow mold with milky white hazing, iridescent pearlescent streaks, or localized stress whitening, the entire production batch is rejected by quality control auditors.
While machine operators frequently misdiagnose both symptoms as “heating problems,” pearlescence and thermal hazing are physically opposing metallurgical phenomena. Pearlescence occurs when PET is stretched too cold (microscopic molecular tearing); thermal hazing occurs when PET is heated too hot (unwanted spherical crystallization).
This factory engineering troubleshooting guide correlates visual optical defects with precise infrared heating zone adjustments, stretch rod velocity calibrations, and pneumatic pre-blow timing on Sailwin linear stretch blow molding machines.
Key Engineering Takeaways
- Pearlescence Means Cold Stretching: When preform temperature drops below the natural stretch boundary (~92°C), high-pressure air overstresses polymer lamellae, creating micro-tears that refract light like mother-of-pearl.
- Thermal Hazing Means Overheating: When preforms exceed 115°C–120°C in the oven tunnel, slow-cooling amorphous PET spontaneously forms opaque crystalline spherulites, resulting in a dull, chalky white wall.
- Pre-Blow Timing Decoupling: Premature pre-blow air stretches the preform before the mechanical stretch rod touches the base, causing off-center base wall thinning and localized whitening.
Having Bottle Cloudiness or Pearlescence on Your Blow Molder?
Submit photos of your defective bottles and preform heating recipes for immediate root-cause parameter diagnosis by Sailwin engineers.
1. Scientific Distinction: Pearlescence vs. Thermal Hazing vs. Moisture Haze
Optical Law: If the haze has a rainbow iridescent sheen, it was blown too cold; if it is chalky white and concentrated at the shoulder, it was blown too hot; if it is uniform throughout, the preform resin was wet.
Review the scientific diagnostic criteria below to identify root causes instantly:
| Defect Phenomenon | Visual Appearance | Physical Polymer Mechanism | Immediate Process Solution |
|---|---|---|---|
| Pearlescence (Overstretching) | Iridescent, pearly white sheen; rough texture inside bottle | PET stretched below orientation temp (<90°C); molecular micro-voiding | Increase lamp power in affected zone by 3%–5%; raise overall oven preheat temp. |
| Thermal Crystallization Haze | Chalky, milky opaque white; smooth wall texture | PET heated above crystallization temp (>115°C); spherulite formation | Reduce infrared lamp voltage; increase oven exhaust cooling air blowers. |
| Moisture Hydrolysis Haze | Uniform dull milky cloudiness across entire bottle | Raw preform resin molded with moisture content > 50 ppm | Preform raw material defect; verify resin dehumidifying drying before injection. |
| Pre-Blow Whitening (Off-Center) | One-sided stress mark or localized corner rupture | Pre-blow pressure triggered too early before rod reaches bottom | Delay pre-blow start angle; reduce pre-blow air pressure (typically 6–10 bar). |
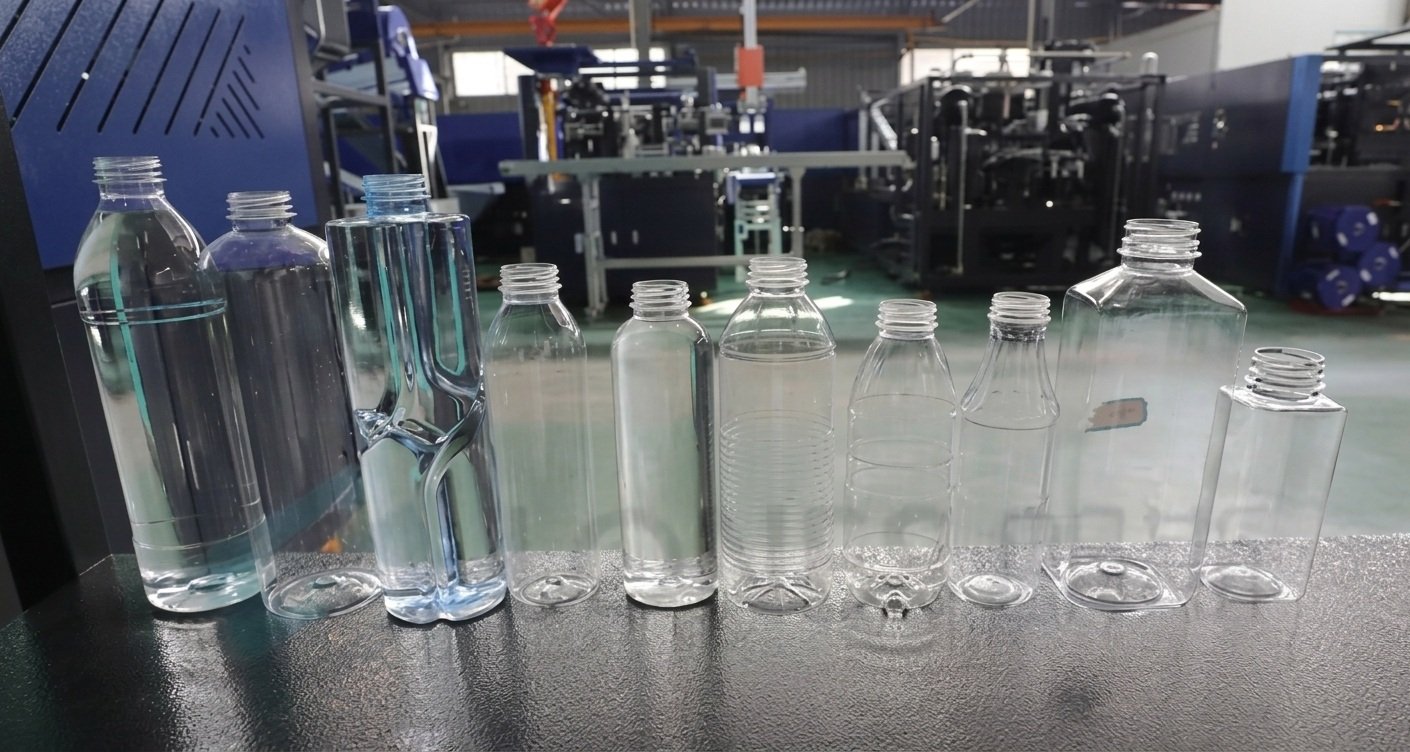
Sailwin Customer Case Study: Water Bottler Eliminates 5.4% Pearlescence Scrap on 500ml Lightweight Line
How a commercial water packaging plant in Jordan solved chronic winter pearlescence by recalibrating infrared oven heating zones.
- Winter ambient temperature dropped factory air to 12°C, causing 5.4% bottle rejection due to base pearlescence.
- Increasing overall oven power caused preform necks to distort and jam mold transfer jaws.
- Bottles with pearlescent bases burst under 6-bar carbonation testing.
- Configured Sailwin zoned infrared heating: raised lower lamp banks by 6% while shielding preform neck finishes with air cooling.
- Recalibrated pneumatic pre-blow timing delay by 0.12 seconds.
- Optimized stretch rod descent speed with servo-driven linear actuator.
- Pearlescence and base fold-over scrap completely plummeted to 0.08%.
- Maintained bottle base drop-test compliance from 1.8 meters.
- Annual resin and production scrap savings exceeded $41,200 USD.
Data source: Sailwin Blow Molding Field Commissioning Record #SW-PET-2026, 2026.
Frequently Asked Questions
SAILWIN MACHINERY · FACTORY-DIRECT PACKAGING SYSTEMS
Achieve Crystal-Clear Bottle Blowing with Sailwin
Sailwin linear servo stretch blow molders integrate precision quartz infrared heating tunnels with 0.1°C thermal stability. Request quote today.
Explore Integrated Packaging Machinery on Sailwin:
• PET Preform Injection Molding Machine – High-speed 140T to 550T systems for multi-cavity bottle preform lines.
• PET Water Bottle Blowing Machine – Linear automatic servo stretch blow molding equipment.
• Liquid Filling Machine & Bottling Line – 3-in-1 rotary monoblocs for drinking water and beverage factories.
• HDPE Extrusion Blow Molding Machine – Industrial continuous blow molding systems for jerrycans and drums.
• Need technical plant advice? Contact our engineering team for free turnkey consultation.



