
Updated: 2026 Engineering Standard · By Sailwin Technical Team
How to Calculate Industrial Chiller Capacity for Blow Molding and Injection Lines (HP vs. kW)
In modern plastics packaging, the industrial water chiller is the thermodynamic backbone of your production facility. Over 65% of the total injection or blow molding cycle time is consumed exclusively by cooling molten polymer below its solidification threshold. Sizing an industrial process chiller too small forces operators to artificially extend cycle times, cutting factory output by 20% to 35% during hot summer months.
Conversely, drastically over-sizing a chiller without variable-speed compressors leads to short-cycling compressor burnout and excessive factory electrical utility bills. On Sailwin blow molding and injection molding lines, exact thermodynamic heat load calculations are required.
This engineering handbook provides the exact thermodynamic formulas, polymer specific heat values (PET, HDPE, PP), and pump flow rate rules necessary to calculate your required chiller tonnage (HP / kW) with zero guesswork.
Key Engineering Takeaways
- Thermodynamic Heat Load Formula: Heat Load Q (kcal/h) = Hourly Resin Throughput (kg/h) × Polymer Specific Heat (Cp) × Temperature Delta (Melt Temp minus Ejection Temp) × Safety Factor (1.20).
- Tonnage Conversion Benchmark: 1 Ton of Refrigeration (TR) = 3.517 kW = 3,024 kcal/h = 12,000 BTU/h. A 100 kg/h PET injection line typically requires approximately 4.5 to 6.0 HP of dedicated chilling capacity.
- Turbulent Water Pumping: Proper heat extraction requires circulating chilled water (10°C–12°C) at a minimum flow rate of 2.4 to 3.0 GPM per ton of cooling to maintain turbulent flow (Re > 4,000) inside mold cavities.
Need Chiller Capacity Sizing for Your Machinery Line?
Submit your hourly resin throughput (kg/h) and polymer grade for complete thermodynamic heat load modeling and chiller specifications.
1. Specific Heat Capacity & Heat Load Formula for Common Plastics
Chiller Sizing Law: HDPE requires twice the cooling energy of PET per kilogram because its semi-crystalline structure releases latent heat during solidification.
Calculate your required cooling capacity using the engineering constants below:
| Polymer Material | Specific Heat Cp (kcal/kg·°C) | Melt Temp (°C) | Ejection Temp (°C) | Cooling Load per kg (kcal/kg) | Required Chiller HP per 100 kg/h |
|---|---|---|---|---|---|
| PET (Bottle Grade) | 0.35 – 0.40 | 280°C | 70°C | 85 – 100 kcal / kg | 4.5 – 5.5 HP Chiller |
| HDPE (Extrusion Grade) | 0.55 – 0.62 | 200°C | 50°C | 130 – 165 kcal / kg | 6.5 – 8.0 HP Chiller |
| PP (Polypropylene) | 0.50 – 0.58 | 220°C | 60°C | 120 – 150 kcal / kg | 6.0 – 7.5 HP Chiller |
| PVC (Rigid) | 0.25 – 0.30 | 180°C | 60°C | 45 – 60 kcal / kg | 2.8 – 3.8 HP Chiller |
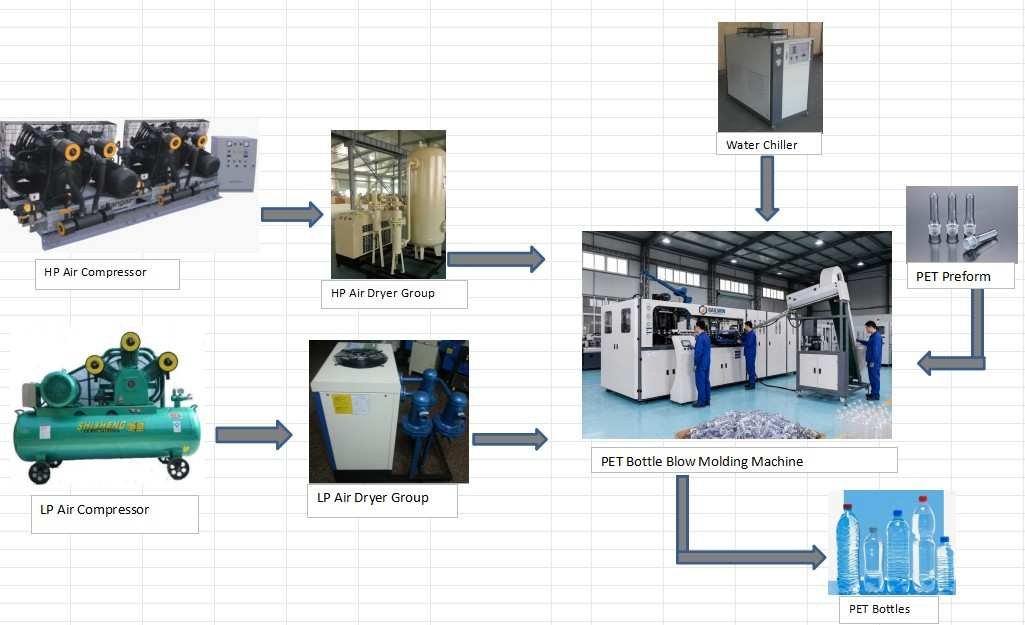
Sailwin Customer Case Study: Packaging Plant Slashes Summer Cycle Times by 28% with Dedicated Process Chiller
How a commercial PET water bottle molder in Dubai overcame summer production slowdowns by sizing a Sailwin 30 HP water-cooled chiller.
- Summer ambient temperature reached 46°C, causing factory cooling tower water to rise to 34°C.
- Blow molder cycle time had to be extended from 2.0s to 2.8s to prevent bottle bottom deformities.
- Annual production dropped by over 1.8 million bottles during peak summer demand.
- Installed Sailwin 30 HP water-cooled industrial screw chiller dedicated exclusively to mold cavities.
- Configured dual-loop manifold delivering constant 9.5°C water at 3.5 bar pressure.
- Integrated anti-condensation dew-point controls to prevent mold sweating.
- Cycle time safely locked at 1.95s year-round regardless of outside ambient heat.
- Total summer bottle output increased by 28.2%.
- Tooling condensation completely eliminated, preventing mold rust.
Data source: Sailwin Engineering Commissioning Log & Client Production File #SW-CHI-2026, 2026.
Frequently Asked Questions
SAILWIN MACHINERY · FACTORY-DIRECT PACKAGING SYSTEMS
Size Your Process Chiller with Sailwin Engineering
Sailwin supplies industrial air-cooled and water-cooled process chillers from 3 HP to 150 HP engineered for packaging lines. Request sizing layout today.
Explore Integrated Packaging Machinery on Sailwin:
• PET Preform Injection Molding Machine – High-speed 140T to 550T systems for multi-cavity bottle preform lines.
• PET Water Bottle Blowing Machine – Linear automatic servo stretch blow molding equipment.
• Liquid Filling Machine & Bottling Line – 3-in-1 rotary monoblocs for drinking water and beverage factories.
• HDPE Extrusion Blow Molding Machine – Industrial continuous blow molding systems for jerrycans and drums.
• Need technical plant advice? Contact our engineering team for free turnkey consultation.



